The datasheet says 316L stainless. That steel is the entry ticket to GMP, not the finish line. A food-grade machine can carry the exact same 316L and still miss the surface finish, crevice-free welds, drainability, and documentation that make a machine qualifiable.
When integrating a packaging machine into a pharmaceutical line, the critical specifications to verify are the ones that never make it onto the marketing sheet. GMP requirements sit on the machine itself, and most of them reduce to a number you can check against a vendor spec before you sign the purchase order.
GMP hygienic design comes down to surfaces that clean fully, joints that hide nothing, and geometry that drains dry. Product-contact roughness must generally sit below 0.8 µm Ra, and electropolishing takes that down to 0.04 µm or less.
The 0.8 µm figure is a universally accepted contact-surface spec, and cleanability shows no measurable difference across the 0.1–0.8 µm band. Pushing to 0.04 µm buys you margin on validation, not a different cleaning regime.
Three construction line items separate a GMP machine from a food-grade one, and each is checkable against a vendor spec:

Joints are where a food machine and a GMP machine diverge most. Every weld should be crevice-free and passivated to remove free iron and restore the chromium oxide layer.
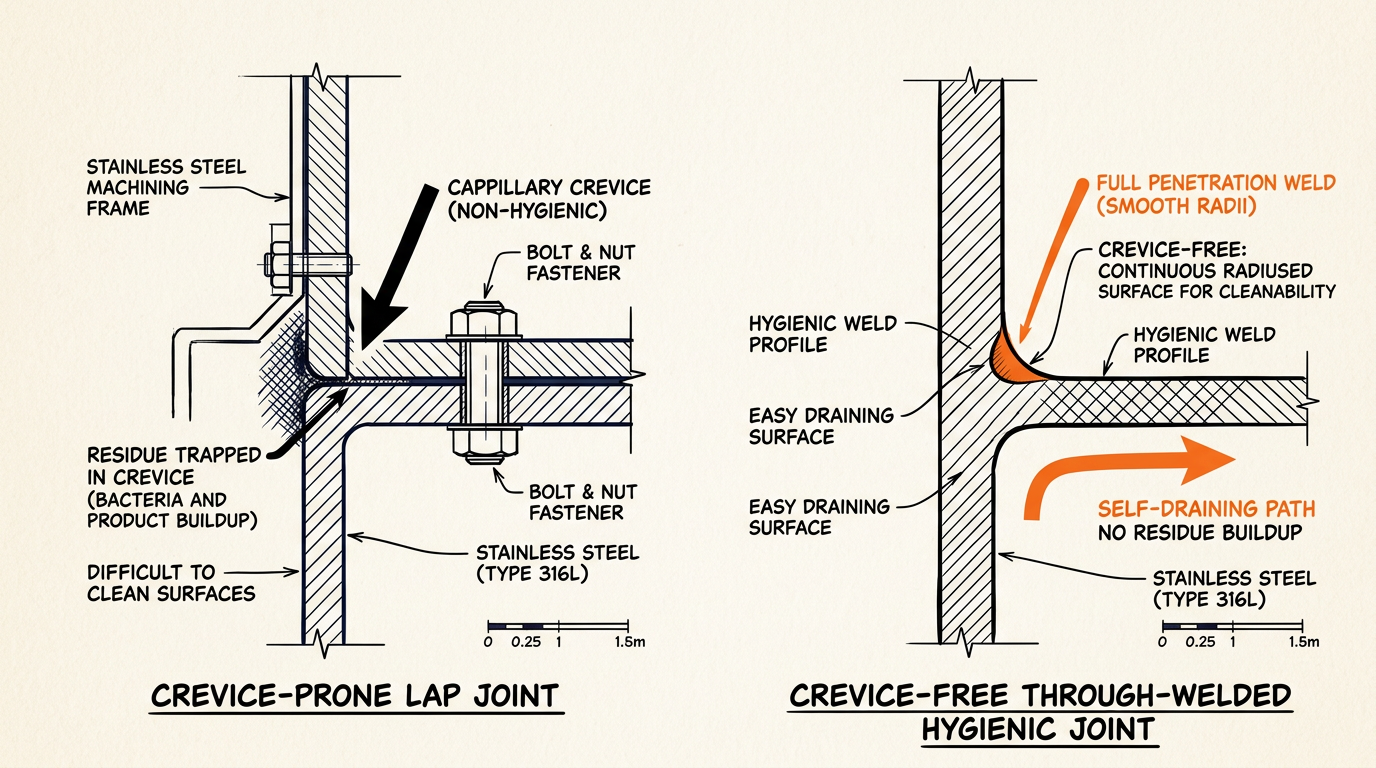
A food-grade line built to wash-down hygiene standards often stops at smooth surfaces and skips the passivation records. Verify the weld map and passivation certificate, not just the visual finish.
Contact parts must be 316L stainless, and the machine builder should carry EN 10204 3.1 material certification for them. The low carbon content plus molybdenum give 316L its resistance to pitting and corrosion; 304 is not recommended for pharmaceutical contact.
Grade alone is necessary but not sufficient. A vendor can quote 316L and still hand you a machine that fails qualification on finish or traceability, so the material claim only holds when it arrives with paperwork.
The specification to verify is the certification chain. Ask for the 3.1 certificate tying each contact component back to its heat number — if the vendor cannot produce it, the “316L” on the datasheet is an assertion, not evidence.
Non-product-contact materials carry requirements of their own. Bearings should be sealed with lifelong lubrication, and any polymer in the product zone must be non-shedding so it never marks or contaminates the pack.
A GMP machine has to prove it comes clean to a defined limit, which means the design must supply accessible, swabbable sampling points at every critical surface. Under actual production conditions, hoppers, nozzles, and seal jaws are the surfaces that accumulate residue and jam a line, so those are the points that get swab-tested or measured by total organic carbon.

The acceptance limit itself has moved on. The long-standing 10 ppm rule — no more than 10 ppm of one product carried into the next — dates to 1993 and was always somewhat arbitrary.
The industry shifted to health-based limits: permitted daily exposure (PDE) and acceptable daily exposure (ADE), formalized in the ISPE Baseline Guide around 2010 and the EMA’s 2012 draft guideline. The European Pharmacopoeia caps rinse-water TOC at 500 ppm, with purified-water conductivity at 4.3 µS/cm at 20 °C.
On the machine, that translates into a swab-recovery test over a 100 cm² area. The acceptable recovery threshold depends on which body you follow:
Changeover is where design either helps or fights you. A machine with tool-free access and a defined line-clearance mode lets an operator prove the line is empty between batches, instead of arguing it. There should be no hidden zones where product can dwell unseen.
For pharmaceutical stick-pack and sachet formats, this changeover discipline is exactly what a purpose-built GMP machine addresses. Soontact’s stick-pack lines are designed around swabbable contact points and no-dwell clearance for this reason.
Validation-readiness is a machine design attribute you verify before purchase, not a service you buy afterward. EU GMP Annex 15 frames qualification as a DQ → IQ → OQ → PQ life cycle, and it puts a specific burden on the equipment supplier: documented evidence.
That evidence package is design specifications, drawings, SOPs, calibration intervals, operating-parameter ranges, and defined sampling points. A machine that ships without it forces you to reverse-engineer qualification from a machine that was never designed to be qualified.
The full IQ/OQ/PQ protocol work is its own exercise — the mechanics of running a horizontal flow packing machine validation walk through what each stage demands. At the machine-selection stage, the question is narrower: does the vendor’s documentation package let you execute that protocol without gaps?
Annex 15 also requires cleaning-validation limits to be scientifically justified, realistic, achievable, and verifiable. A machine that cannot be sampled at its critical surfaces cannot satisfy that clause, which is why sampling-point access is a validation requirement, not a cleaning convenience.
A GMP packaging machine must record what it did, prove who did it, and keep that record tamper-evident. Where the controls handle electronic batch data, 21 CFR Part 11 sets the bar with three controls the vendor has to demonstrate:
The audit trail is the requirement most often under-specified at purchase, so confirm it captures parameter changes at the field level, not just batch start and stop.
Traceability closes the loop from machine to pack. When you evaluate a machine vendor, treat the documentation package as a line item with the same weight as throughput. The supplier-selection checklist that works for a VFFS line applies here, with data-integrity evidence added.
Verify the finish, the welds, the drainage, and the documentation before you verify the steel grade. The grade is the one thing a food-grade machine and a GMP machine already share.
The most common failure I see is a specifier who confirms “316L construction,” checks the box, and stops. They never ask for the Ra measurement, the passivation record, the swab-point map, or the Annex 15 evidence package.
A machine is GMP-ready when every requirement category resolves to a number or a document you can hold, not a claim you have to trust. Walk into the evaluation with that checklist and confirm each line against the vendor’s own paperwork before you commit. The gap between a food machine and a pharma machine is measured in exactly those verifications.
